
Brass is soft, often polished or lacquered, so mark quality depends on wavelength, surface coating, fixture and cleaning — not wattage. This buyer's guide explains how 1064nm and 455nm lasers behave on bare versus coated brass, compares the two wavelengths, and shows how to test brass samples before you specify a brass engraving machine.
Brass nameplates, gift items, instrument dials and switch panels usually arrive already polished or lacquered. That finish is what makes the part look expensive, and it is also what makes laser marking tricky. Buyers often assume that a higher wattage number on the label automatically gives a darker, sharper mark. On brass, it does not work that way. Mark quality is governed by wavelength, surface coating, fixture stability and post-mark cleaning — the four variables this guide explains.
Key takeaways: a 1064nm laser marks bare metal; a 455nm diode laser marks coated or anodised surfaces rather than bare metal. Polished and lacquered brass needs its coating identified before you choose a brass engraving machine, and the wattage printed on the housing is not the deciding factor.
Why brass behaves differently from steel or aluminium
Brass is soft and reflective. When a laser hits bare brass, three things happen at once: the surface reflects a large share of the beam, the metal conducts heat away from the spot quickly, and the small amount of energy that is absorbed has to create a visible mark before the heat spreads. Wattage alone does not overcome reflection. Wavelength does, because different metals absorb different wavelengths to different degrees.
The second factor is the finish. A lacquered nameplate, a clear-coated instrument bezel and a bare machined blank are three different materials from the laser’s point of view. If you choose a machine by wattage and ignore the coating, the mark may be pale on one batch and burn through the lacquer on the next.
Wavelength: the first decision
Two laser types are commonly sold for brass work, and they are not interchangeable.
1064nm fibre laser
A 1064nm laser marks bare metal. It is absorbed by the metal surface itself, so it works on unlacquered brass, stainless steel and aluminium without a coating to burn. A machine built around this wavelength, such as the WAINLUX K8-1064nm laser engraving machine, is designed for bare-metal marking rather than coated surfaces.
455nm diode laser
A 455nm diode laser marks coated or anodised surfaces rather than bare metal. It is the practical choice when the brass part carries a lacquer, paint or anodised layer that the beam can react with. The XN001-3W is a 3W 455nm machine that marks coated metal only, so it should not be specified for bare brass.
| Comparison point | 455nm diode laser | 1064nm laser |
|---|---|---|
| What it marks | Coated or anodised surfaces, not bare metal | Bare metal |
| Behaviour on polished bare brass | Not intended; the beam has no coating layer to act on | Absorbed by the metal surface |
| Behaviour on lacquered brass | Acts on the coating | The coating is part of what the process must account for |
| Typical role in a brass workflow | Marking coated blanks and mixed materials | Marking bare brass parts and plates |
| Example in this range | XN001-3W (3W) | WAINLUX K8-1064nm; the 1064nm head of the X1-20W dual-laser |
The two wavelengths address different substrates. Neither replaces the other on the same brass condition.
If your brass is both bare and coated
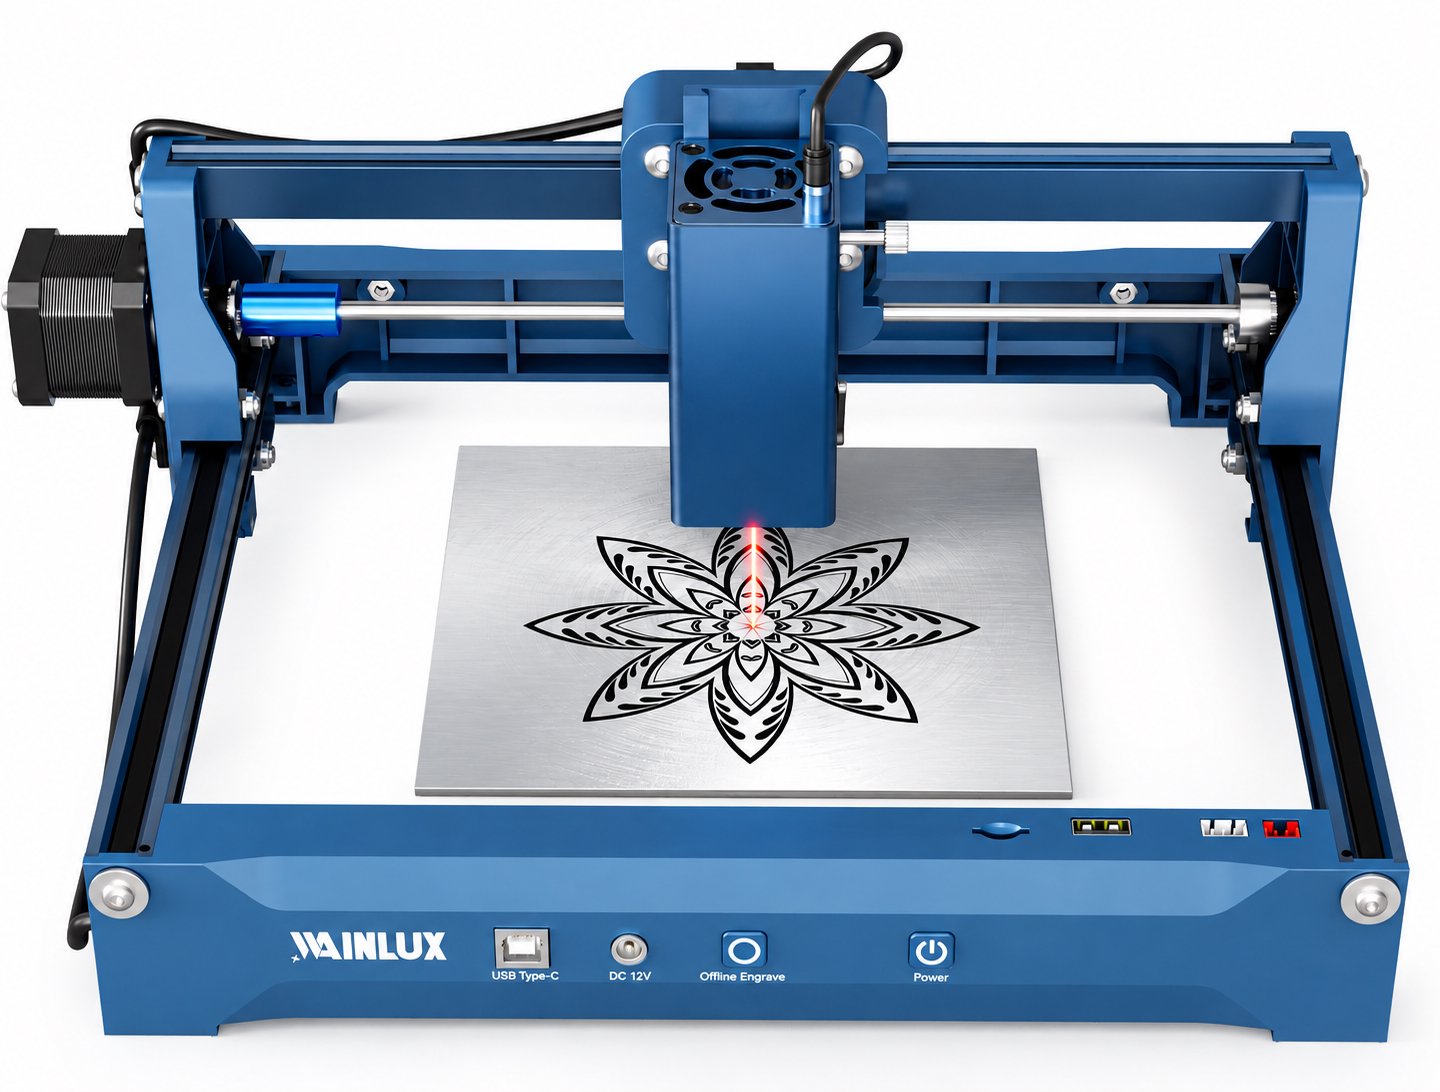
A workshop that receives a mix of bare blanks and lacquered plates, or that also marks wood, leather, acrylic and coated metal, has to run both processes. A dual-laser configuration solves this without buying two machines. The WAINLUX X1-20W dual-laser engraving machine carries one 455nm head and one 1064nm head, with a 30 x 30 cm working area. It handles wood, leather, acrylic, coated metal and bare-metal marking, and it can work offline from WiFi, USB-C or a TF card. For a buyer who must mark brass parts and gift packaging on the same bench, that combination removes the need to route bare-metal jobs elsewhere.
Fixture: the variable buyers underestimate
Once the wavelength matches the substrate, positional repeatability decides whether the mark lands where the drawing says it should. Brass nameplates usually carry fine text and serial data, so a shifted part means a scrapped plate.
The WAINLUX K8-1064nm illustrates the numbers that matter here: an 8 x 8 cm working area, 0.01 mm positioning precision and an engraving depth range of 0.1–1 mm. Positioning precision describes how accurately the system places the beam, not how deep it cuts. Depth is a separate parameter and is set according to the mark you want. A rotary roller is available as an option for cylindrical brass work such as rings or tubes, and an air purifier is offered for the fumes produced when a coating is marked.
On the machine side, the K8 runs at up to 2000 mm/s and connects over USB, WiFi or Bluetooth. It works from Windows without professional software, which matters if the operator preparing plates is not a trained laser technician. The unit measures 190 x 286 x 313 mm and weighs 4.4 kg, and it ships with sample blanks so that a buyer can test the process on real material before committing a production batch.
Testing brass samples: a numbered procedure
Do not approve a brass engraving machine from a catalogue photo. Approve it from marked parts that match your production condition. Supplier-provided sample blanks make this practical, because they let you run the comparison below on the same material you will buy.
- Confirm the brass condition of the production part: bare, polished, lacquered, painted or plated. Record it, because the wavelength decision follows from this.
- Confirm the wavelength of the machine you are evaluating — 1064nm for bare metal, 455nm for coated or anodised surfaces.
- Mark the same artwork on a sample blank: fine text at the smallest size you use, plus any logo or serial field.
- Inspect the mark under the same lighting your customer will use. Check edge sharpness, contrast and whether the coating is intact around the mark.
- Clean the marked part with your normal post-process wipe and inspect again. Cleaning is where marginal marks disappear.
- Repeat the mark on several blanks from the same batch and compare position. This shows whether the fixture holds the part repeatably.
- Only then approve the machine for that brass condition, and keep the approved sample as a reference for incoming checks.
Tip: if your brass is lacquered, specify the mark on the coating, not through it. Marking through a lacquer layer to reach the metal below often damages the surrounding finish, and the failure only shows up after handling.
Cleaning, handling and what buyers should verify
A laser mark on brass is a surface change, not a sticker. Its final appearance is settled during cleaning, so the wiping method used on the line is part of the specification. Ask the supplier to state which cleaning step the sample mark is expected to survive, and test it on the sample blanks rather than on finished goods.
Thickness and flatness of the blank also affect results. A bowed plate sits unevenly under the beam, which changes focus across the surface and makes the mark inconsistent from edge to edge. For flat nameplates this is usually solved by the fixture; for cylindrical parts it is the reason a rotary roller option exists.
When comparing suppliers, ask for the sample-blank policy in writing. A supplier willing to send blanks for your own test is giving you a measurable basis for the decision. WAINLUX has been manufacturing laser equipment since 1998, holds an ISO9001 company-level certificate, works through OEM/ODM projects and exports to 50+ countries, which is relevant when you are qualifying a supplier rather than a single unit.
Specification summary for the two brass-ready options
| Item | WAINLUX K8-1064nm | WAINLUX X1-20W dual-laser |
|---|---|---|
| Laser configuration | 1064nm | One 455nm head and one 1064nm head |
| Working area | 8 x 8 cm | 30 x 30 cm |
| Positioning precision | 0.01 mm | Not stated in this summary |
| Engraving depth | 0.1–1 mm | Not stated in this summary |
| Speed | Up to 2000 mm/s | Not stated in this summary |
| Connectivity | USB, WiFi, Bluetooth | WiFi, USB-C, TF-card offline working |
| Software | Works from Windows without professional software | Offline working supported |
| Materials covered | Bare-metal marking | Wood, leather, acrylic, coated metal and bare-metal marking |
| Machine size | 190 x 286 x 313 mm | Not stated in this summary |
| Weight | 4.4 kg | Not stated in this summary |
| Included with machine | Sample blanks; optional rotary roller and air purifier | Not stated in this summary |
Fields marked “not stated in this summary” should be confirmed with the supplier for your specific configuration rather than assumed.
Frequently asked questions
Can I mark bare brass with a 455nm diode laser?
A 455nm diode laser marks coated or anodised surfaces rather than bare metal. For bare brass the matching configuration is a 1064nm laser.
Does higher wattage give a darker mark on brass?
No. Absorption at the working wavelength, the surface coating and the focus stability of the fixture determine the result. Wattage is one input among several.
What if my parts are cylindrical?
The WAINLUX K8-1064nm supports an optional rotary roller for cylindrical work. Confirm the diameter range you need with the supplier before ordering.
Can one machine cover bare and coated brass?
A dual-laser machine such as the X1-20W, with a 455nm head and a 1064nm head, covers both coated and bare-metal marking within its 30 x 30 cm working area.
Next step
Send us the brass condition (bare, polished, lacquered or plated), the part size and the smallest text or logo you need to mark. We will confirm which wavelength fits and arrange sample blanks so you can test the mark before you order. Tell us your target quantity and delivery country, and we will reply with the configuration and commercial terms.